- 0091-022-66362797 / +91-9821025398
- ngchouhan@gmail.com / ganpatmetal03@gmail.com
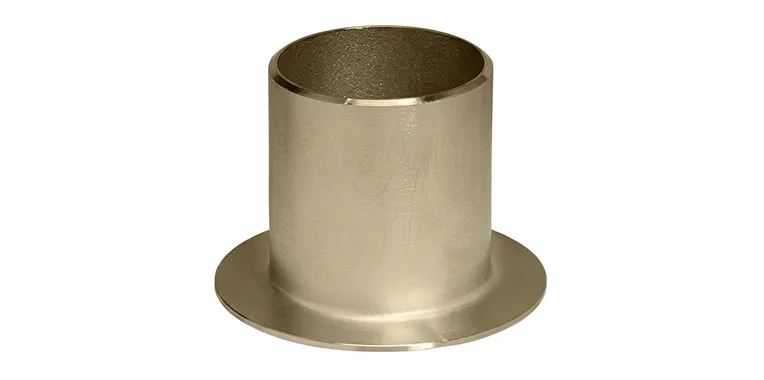
Ganpat Metal manufactures and supplies high-performance Super Duplex Stainless Steel Butt Weld Fittings conforming to ASTM A815 / ASME SA815 Grade WPS32750 (Alloy 2507) and WPS32760 (Zeron 100). Super duplex alloys provide an exceptional combination of high tensile and yield strength coupled with supreme resistance to pitting, crevice corrosion, and erosion in warm aggressive saline and sour chloride media, guaranteed by a Pitting Resistance Equivalent Number (PREN) ≥ 42.
Our super duplex butt weld fittings range covers elbows, tees, reducers, end caps, and stub ends manufactured under stringent metallurgical temperature controls. Following hot or cold forming, fittings undergo solution heat treatment at 1100°C–1140°C with instantaneous water quenching to eliminate sigma or chi intermetallic phases and maintain a 50/50 austenite-ferrite phase balance.
Designed for severe offshore oil & gas topsides, subsea tiebacks, desalination plants, and chemical process piping, all super duplex fittings conform to ASME B16.9 and NORSOK M-650 / M-630 MDS D53 standards, backed by 100% NDT inspection and EN 10204 Type 3.1 certification.
GM handles enquiries for Super Duplex Stainless Steel Butt Weld Fittings where buyers need to match fitting types (elbows, tees, reducers, end caps), nominal pipe sizes (NPS / DN), wall thickness schedules, and material grade to piping isometric drawings or project purchase specifications. The supplied inventory covers seamless and 100% X-ray welded fittings from 1/2" NB up to 48" NB across all schedules from Sch 10S to Sch XXS.
Grade selection should be based on the design pressure, service temperature, fluid media corrosivity, and mechanical strength requirements of the piping system. Buyers should also confirm the applicable manufacturing standard (ASME B16.9 / MSS-SP-43), weld bevel preparation (ASME B16.25), supplementary inspection requirements (radiography, PMI, hydrotest), and test documentation before finalizing an order.
| Parameter | Specification |
|---|---|
| Standard Specifications | ASTM A815 / ASME SA815, ASME B16.9, MSS-SP-43, NORSOK M-630 MDS D53 |
| Available Grades | ASTM A815 WPS32750 (2507), ASTM A815 WPS32760 (Zeron 100) |
| Fitting Types | 90°/45° LR & SR Elbows, Equal/Reducing Tees, Concentric/Eccentric Reducers, Caps |
| Size Range | 1/2" NB to 48" NB (Seamless up to 24", Welded up to 48") |
| Schedule / Thickness | Sch 10S, Sch 40S, Sch 80S, Sch 160, Sch XXS |
| Pitting Index | PREN = %Cr + 3.3(%Mo + 0.5%W) + 16(%N) ≥ 42 |
| Impact Toughness | Charpy V-Notch impact testing at -46°C (min 80 J average, 60 J single) |
| Corrosion Test | ASTM G48 Method A Ferric Chloride Pitting Test at 50°C (no pitting) |
| Testing & Certification | Microstructure phase ratio (ASTM E562 40-60%), PMI, 100% RT/UT |
| Documentation | EN 10204 Type 3.1 / 3.2 MTC, NACE MR0175 / ISO 15156, NORSOK MDS D53 |
Standard chemical composition limits conform to international metallurgical standards.
| Grade | C max | Cr | Ni | Mo | N | W / Cu | Fe |
|---|---|---|---|---|---|---|---|
| WPS32750 (2507) | 0.030 | 24.0 – 26.0 | 6.0 – 8.0 | 3.0 – 5.0 | 0.24 – 0.32 | Cu 0.5 max | Balance |
| WPS32760 (Zeron 100) | 0.030 | 24.0 – 26.0 | 6.0 – 8.0 | 3.0 – 4.0 | 0.20 – 0.30 | W 0.5–1.0, Cu 0.5–1.0 | Balance |
Minimum mechanical property requirements in designated standard delivery condition:
| Grade | Tensile Strength (min) | Yield Strength 0.2% (min) | Elongation (min) | Hardness (max) |
|---|---|---|---|---|
| WPS32750 | 750 MPa (109 ksi) | 550 MPa (80 ksi) | 25% | 310 HBW / 32 HRC |
| WPS32760 | 750 MPa (109 ksi) | 550 MPa (80 ksi) | 25% | 310 HBW / 32 HRC |
| Standard / Country | Designation |
|---|---|
| ASTM A815 WPS32750 | UNS S32750 • W.Nr. 1.4410 • EN X2CrNiMoN25-7-4 • Sandvik SAF 2507 |
| ASTM A815 WPS32760 | UNS S32760 • W.Nr. 1.4501 • EN X2CrNiMoCuWN25-7-4 • Zeron 100 |
| Form / Type | Size Range | Length / Dimensions | Condition / Standard |
|---|---|---|---|
| 90° Long Radius (LR) Elbow | 1/2" to 48" NB (DN15 - DN1200) | Sch 5S to Sch XXS | ASME B16.9 / R = 1.5D |
| 45° Long Radius (LR) Elbow | 1/2" to 48" NB (DN15 - DN1200) | Sch 5S to Sch XXS | ASME B16.9 / Standard Radius |
| 90° Short Radius (SR) Elbow | 1/2" to 36" NB (DN15 - DN900) | Sch 10S to Sch XXS | ASME B16.9 / R = 1.0D |
| Equal / Straight Tee | 1/2" to 48" NB (DN15 - DN1200) | Sch 5S to Sch XXS | ASME B16.9 / Center-to-End C = M |
| Reducing Tee | 1/2" x 3/8" to 48" x 40" NB | Sch 5S to Sch XXS | ASME B16.9 / Branch Dimension M |
| Concentric Reducer | 1/2" x 3/8" to 48" x 40" NB | Sch 5S to Sch XXS | ASME B16.9 / In-line Center Flow Axis |
| Eccentric Reducer | 1/2" x 3/8" to 48" x 40" NB | Sch 5S to Sch XXS | ASME B16.9 / Flat Side for Horizontal Lines |
| End Cap | 1/2" to 48" NB (DN15 - DN1200) | Sch 5S to Sch XXS | ASME B16.9 / Ellipsoidal Head Profile |
| Stub End (Lap Joint) | 1/2" to 24" NB (DN15 - DN600) | Sch 5S to Sch 80 | MSS-SP-43 / ASME B16.9 Short/Long Pattern |
Custom dimensions, special cuts, and tailored surface conditions available on request.
Estimate butt weld fitting weights by fitting type, nominal pipe size (NPS) and schedule.
Ganpat Metal manufactures and supplies certified Super Duplex Stainless Steel Butt Weld Fittings for industrial buyers across India. All materials are sourced from premium quality mills, fully tested for chemistry, mechanical properties, and dimensional tolerances, and supplied with complete traceable Mill Test Certificates.
Whether you require standard stock dimensions or customized sizes, Ganpat Metal maintains deep inventories in Mumbai and provides rapid dispatch, custom cut-to-length services, and third-party inspection support.
 India
 UAE
 Saudi Arabia
 Oman
 Australia
 Malaysia
 Singapore
 Bangladesh
 Egypt
 Brazil
 Russia
 Kazakhstan
| Requirement | Details to Provide |
|---|---|
| Fitting Type | 90°/45° LR Elbow, Equal Tee, Reducing Tee, Reducer, Cap, Stub End |
| Grade | ASTM A815 WPS32750 (2507) or WPS32760 (Zeron 100) |
| Size (NPS / DN) | 1/2" NB to 48" NB |
| Schedule / Wall | Sch 10S, Sch 40S, Sch 80S, Sch 160, Sch XXS |
| Construction | Seamless or 100% X-Ray Welded (ASME B16.9) |
| End Preparation | Beveled Ends (ASME B16.25) or Plain Square Cut |
| Pitting Test | ASTM G48 Method A test at 50°C requirement |
| Documentation | EN 10204 Type 3.1 / 3.2 MTC with Ferrite, Impact & PMI reports |